Hey everyone, Sarah here from the slant bed lathe team—if you’ve ever walked our booth at a machining show, you’ve probably heard me ramble about how our machines aren’t just “that CNC lathe that sits on an angle.” Today’s question is one I get at least twice a week, usually from small shop owners or new machinists testing the waters: Can a slant bed lathe actually do milling? Let’s cut through the confusion, because the answer isn’t a simple yes or no—and as someone who’s spent the last 7 years selling these machines, I’ve seen firsthand where it works, where it falls short, and when it’s actually worth trying. Slant Bed Lathe

First, let’s do a quick refresh on what a slant bed lathe even is, because I’ve had so many customers mix it up with a straight bed lathe. Straight beds are the old-school ones that sit flat, with the turret or tool post facing up, which means chips go everywhere and you have to crane your neck to check deep cuts. Slant beds? They’re set at a 30 or 45 degree angle—super practical for slinging chips down and out, better chip evacuation, stiffer spindle rigidity, and easier access to the work zone for operators. That angle is key here, because it’s also what makes people wonder if milling might be possible.
Milling, for anyone who’s not 100% fluent in machining lingo, is when you spin a tool (like an end mill or drill) to cut material on multiple axes, not just spinning the workpiece like a lathe does. So at its core, lathes turn parts, mills cut shapes, holes, or features on sides of parts—but hybrid operations are a big thing now, especially for small shops that don’t want to buy a whole separate mill.
So back to the question: Can our slant bed lathes do milling? The short answer is: Sort of, but only specific types of milling. Let’s talk about what’s actually possible on a standard slant bed lathe (not one that’s a total Frankenstein mod, though I’ve seen those too). The main tools on a slant bed lathe live in a turret—usually a 12-station or 16-station live tool turret, right? Live tools are the ones that spin on the turret, so they’re not just holding a static lathe tool like a turning insert. If your slant bed lathe has live tooling, that’s where the milling magic starts.
What can you actually do with those live tools? Small, light-duty milling operations—think drilling holes perpendicular to the lathe’s main spindle, tapping cross holes (like if you have a 2-inch shaft and need a 1/4-inch threaded hole that runs straight across it), slotting tiny keyways on the side of a shaft, or even light contour milling for simple faces. I sold our most popular mid-sized slant bed lathe to a guy in Cleveland last month, and he used it to make small valve bodies for farm equipment—he drilled 4 cross holes and milled flat sides for gaskets all on the lathe, no need to move the part to a mill. That’s the sweet spot here.
But here’s where people get overexcited: You can’t do heavy milling on a standard slant bed lathe. Let’s be real—those live tool turrets are built for small loads. If you try to hog out a 1-inch pocket of steel at full speed with a 1-inch end mill, you’re gonna bend the tool, break the spindle, or end up with a part that’s way off spec. Slant beds are rigid for turning, but milling puts side and radial loads on the tool and spindle that most standard slant bed live tool setups aren’t engineered for. I had a customer in Chicago call me last year panicking because he tried to mill a 3-inch wide flat on a 6-inch aluminum shaft on our entry-level slant bed lathe. He stripped a live tool motor and bent the turret mount before he got halfway done. Lesson learned: Know your machine’s limits.
Another big point: It all comes down to the control and axis configuration of your slant bed lathe. Most modern slant bed lathes run on Fanuc or Siemens controls, which can be programmed to handle live tool operations, but only if they have the right axis. You need a CNC with at least 4 axes for proper milling—X, Z for lathe turning, and B or Y for the live tool to move in the horizontal plane. Some cheaper entry-level slant beds only have basic 3-axis setups, so their live tooling is limited to just drilling and tapping, no contouring or milling complex shapes. That’s why I always tell new buyers to ask: “Does this lathe have full Y-axis live tooling or just basic cross drilling?” Because that’s the difference between “I can do a couple of side holes” and “I can do simple 2D milling.”
Wait, what about Swiss-type slant bed lathes? Oh, those are a whole different beast. Swiss lathes are smaller, super precise, and popular for medical parts, electronics connectors, and tiny aerospace components. A lot of Swiss-type slant beds come standard with live tooling that can do light milling operations all in one setup. I worked with a company that makes tiny surgical pins a while back—they used a Swiss slant bed lathe to turn the pin, mill the flat sections, drill tiny cross holes, and even tap threads, all without moving the part once. That cuts their setup time by like 80% compared to using a separate mill. That’s where this combo really shines—small, high-precision parts where you don’t need heavy milling, just multiple operations done in one machine.
But let’s get real about the downsides too, because I’m not here to oversell. Milling on a slant bed lathe is never going to replace a full-size vertical or horizontal mill for heavy, high-volume milling. If you’re running 1000 aluminum parts a week that need deep pockets or complex 3D contours, a slant bed lathe’s live tooling will be too slow, too limited, and you’ll end up wasting money on downtime and broken tools. Also, setup for milling on a lathe is different—you have to make sure the live tool is trued up, the workholding is secured extra tight (since milling creates more vibration than turning), and you’re programming for the live axis correctly, which takes a little extra knowledge if you’re only used to turning. I always offer training to our customers who want to use their slant beds for milling—because it’s not just plug and play, it’s knowing how to adjust feeds and speeds for live tools, not just turning inserts.
Another common mistake I see: People think “slant bed = perfect for milling” just because of the angle. No, the slant bed’s main job is for chip evacuation and rigidity for turning, not milling. Some higher-end slant beds are built with reinforced spindles and heavy-duty live tool motors to handle more milling, but even then, they’re designed as lathes first, mills second. So if your main workflow is mostly turning parts with occasional light milling, a slant bed lathe with live tooling is a great investment. If your main job is milling or heavy milling, buy a mill, not a lathe.
Wait, let’s talk about examples of actual use cases, because numbers and stories stick better than theory. A customer of ours in Detroit makes small automotive brackets. They have two mid-sized slant bed lathes with full Y-axis live tooling. Before, they would turn the bracket on a straight bed lathe, move it to a mill to drill the mounting holes and mill the flat surfaces, then move it to a secondary operation to tap those holes. Total cycle time: 12 minutes per bracket. Now they do all of it on the slant bed lathe: turn, drill, mill, tap, all in 4 minutes. That’s a 67% time save, no extra handling, less risk of damaging parts during transfers. That’s the win when it works.
Another example: A hobbyist or small job shop owner who needs to make custom parts once or twice a month, not high-volume. They have a slant bed lathe for turning their standard parts, and when they need a part that has a few side features, they just swap out a turning insert for a live end mill, program a quick milling operation, and they’re done. Way cheaper than buying a separate mill just for occasional side work.
So putting it all together: Yes, a slant bed lathe can be used for milling operations—but only specific milling operations. It’s not a replacement for a dedicated mill, but it’s an amazing hybrid tool that fills a huge gap for small shops, low-to-medium volume parts, and operations that combine turning and light side work. The key factors are: does your slant bed lathe have full live tooling with Y-axis, is it built with enough rigidity for the milling loads you need, and are you okay with sticking to light milling tasks, not heavy hogging or complex 3D shapes.
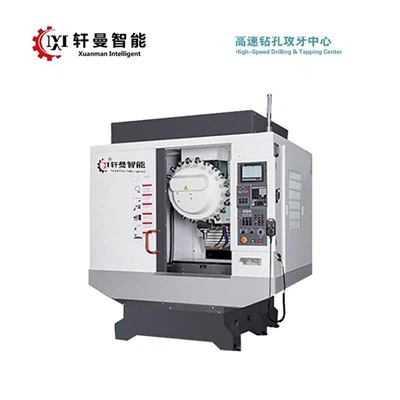
I always tell customers when they come to me: “Tell me what parts you run, how much volume, what features you need.” If it’s mostly turning with a few cross holes or small flats, slant bed with live tool is perfect. If it’s 50% milling or heavy steel cuts, go get a mill. That’s the call you have to make.
CNC Turning Machine If you’re shopping around for a slant bed lathe and want to ask more about live tooling, milling capabilities, or even the different models we have, just reach out to our team. We can walk you through setups, feed rates, use cases that match your work, no pressure, no sales pitch—just straight talk, which is what we’ve built our business on. Don’t waste money on a machine that doesn’t fit your needs, and don’t write off a slant bed lathe as only a turning machine—you might be missing out on cutting cycle times and simplifying your workflow.
References
- Machining Fundamentals: Lathe vs Milling Operations, Modern Machine Shop, 2022
- Slant Bed Lathe Design and Capabilities, American Machinist, 2021
- Live Tooling Application Guidelines for CNC Lathes, Haas Automation Technical Manual, 2023
- Hybrid Lathe-Mill Workflows for Small Job Shops, SME Manufacturing Engineering, 2022
Jiangsu Xuanman Intelligent Equipment Co., Ltd.
We’re well-known as one of the leading slant bed lathe manufacturers in China, featured by quality products and low price. Please rest assured to buy discount slant bed lathe made in China here from our factory. We also accept customized orders.
Address: No. 1-1, Weier Road, Jieji Equipment Manufacturing Industrial Park, Sihong County, Suqian City, Jiangsu Province, China
E-mail: jsxmzn@163.com
WebSite: https://www.xm-cnc.com/
