Hey everyone, let’s cut to the chase – if you’re in the dairy game, you’ve probably wasted more than a few hours messing around with offline testing. You know the drill: pull a sample from the tank, haul it to the lab, wait an hour or two for results, by which time that batch you were tweaking is already half-fermented or off-specific gravity thanks to temperature shifts or uneven mixing. As an in-line density meter supplier, I get it – we’ve all been there, staring at a batch that’s either too watery or too thick because we didn’t adjust fast enough. But can an in-line density meter actually work for dairy? Spoiler alert: yeah, it’s not just a gimmick – it’s a game-changer for 90% of dairy operations, and I’m here to break down why, no fancy jargon required. In-line Density Meter
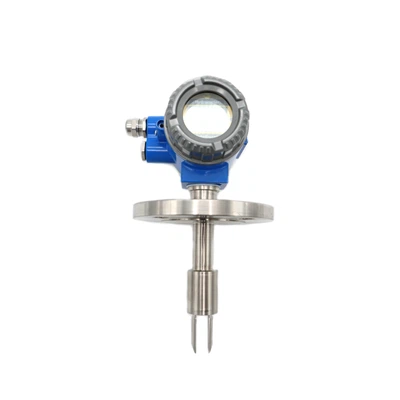
First, let’s get on the same page about what an in-line density meter is, in plain English. It’s a sensor that’s plumbed right into your pipeline, so it’s measuring every drop of product as it flows by – no sampling, no waiting, no human error from mislabeling or forgetting to cool a sample before testing. For dairy, that means it’s measuring the density of milk, cream, yogurt, cheese curd slurry, even ice cream mix in real time. Density and dairy go hand in hand because almost every key quality metric ties back to it. Let’s start with the basics: whole milk is roughly 1.030-1.035 g/cm³ at 20°C, right? Skim milk is a little denser (1.035-1.040 g/cm³) because fat is lighter than water, so removing fat bumps up density. Cream is way less dense, like 0.995-1.010 g/cm³, so blending milk and cream to hit a specific fat content – that’s where density comes in. No more guessing if you poured enough cream or whole milk for that 2% fat line; the in-line meter spits out a reading every second, and your system adjusts the flow valves automatically. I’ve seen small cheese creameries cut blend time by 70% just by adding a basic in-line density meter, no extra staff needed.
But wait, I know what some of you are thinking: dairy products are chunky, messy, prone to fouling, and temperature-sensitive. Won’t that wreck the meter? Let’s address the big myths first, because that’s where a lot of dairy guys get stuck. Myth #1: In-line meters can’t handle viscous dairy products like cheese curd or yogurt. No, modern meters are built with self-cleaning designs – we use a tuned vibrating tube, basically a U-shape that vibrates at a frequency specific to whatever’s flowing through it. Thick slurry? It just changes the vibration frequency, same as liquid, as long as the sensor is kept clean. Oh, and fouling – that’s real, but we build our meters with wetted parts that are easy to wipe down, and a small CIP (clean-in-place) cycle that runs on schedule, so you don’t have to take the sensor out of the line for manual cleaning every shift. I work with a small yogurt plant in Wisconsin that runs their density meter on Greek yogurt mix, which is super thick and sticky, and they’ve only had to do a deep clean once a week – the CIP cycle handles the rest, no downtime.
Myth #2: Temperature throws density readings off too much. Fair point – density changes with temp, about 0.0002 g/cm³ per °C for milk. But all good in-line density meters (yep, including ours) have built-in temperature compensation. So if the product flowing is 40°C instead of 20, the meter automatically adjusts the density reading to what it would be at that reference temp, so you’re not getting false low readings. That’s non-negotiable for dairy, because raw milk comes in at different temps depending on the cow, the time of year, and how long it’s been in the silo. Without temp compensation, you’d be adjusting fat blends based on a wrong number – total waste of time and milk.
Now, let’s get into actual use cases because numbers don’t lie, and I don’t do “it’s good in theory.” Let’s start with raw milk receiving – this is where every dairy’s profit starts. When a milk hauler drops off a tanker full of raw milk, you need to test its fat content, solids-not-fat (SNF), and density to make sure you’re paying the right price (or rejecting it if it’s adulterated, which is a huge problem). Right now, most plants use a hydrometer in the lab, or a manual test, which takes 15 minutes per sample. With an in-line density meter plumbed at the tanker discharge, you can test every gallon as it flows in, and if the density is off, you know right away – either the milk is diluted with water (common scam that costs dairy plants thousands a year) or the fat/SNF is low, so you can reject the load before you even unload it. I had a customer a couple years ago – a mid-sized dairy in Ohio – who told us their density meter caught three diluted milk loads in the first month, saving them like $12,000 total. That’s not chump change for a plant.
Next up: blending for finished products. Let’s say you make 2% fat milk. You need to mix whole milk, skim milk, and cream just right to hit that exact fat percentage. Before in-line meters, operators would test every batch with a Babcock test, which is tedious and takes forever. If you messed up, you either had to rework the batch (wasting milk, time, energy) or sell it as “adjusted” at a lower price, eating into profits. With an in-line density meter, the control system adjusts the flow of each component in real time, so you hit 2% fat on the first try, every time. And for higher-end products like organic milk or grass-fed milk, consistency is everything – customers notice if one batch is thicker than the last, and they’ll switch brands. Our customers who do organic report a 95% consistency rate for their fat blends, up from like 70% before they added the meter.
Cheese making? Oh, that’s where density is a big one for curd yield. When you make cheese, the curd is separated from whey, and the density of the curd slurry tells you how much fat and protein are in the curd – which directly translates to how much finished cheese you get. If you mess with the curd cutting time or the amount of renin, density shifts, and your yield drops. One of our cheese plant customers in Vermont told us they used to have a 5-8% variation in cheese yield per batch; after installing the in-line density meter to monitor curd density, that variation dropped to less than 2%, so they’re making $30k more in cheese every year on the same amount of milk. That’s the real benefit, not just “faster testing.”
What about the big, messy stuff: CIP cycles and sanitation? Dairy plants have to be 100% sanitary, no exceptions. Our in-line density meters are made with 316L stainless steel, which is the industry standard for food processing, and the wetted surfaces are polished to a smooth finish so milk can’t stick or grow bacteria. Also, during CIP cycles, the meter can tell if the water, caustic, and acid solutions are at the correct concentration – because if the caustic is too weak, it won’t clean the lines; too strong, it’s a safety hazard and wastes chemicals. A lot of plants test CIP solutions manually, but an in-line density meter can do it automatically, so you don’t have to send a lab tech to the line every hour to test. That’s another big labor saver.
Wait, but let’s be real – it’s not for every dairy operation. If you’re a small family creamery that makes artisanal cheese in 50-gallon batches, and you only produce 100 gallons a day, maybe a $10k in-line meter isn’t worth it – you can get by with manual testing for now. But if you’re producing 10,000+ gallons a day, or you’re looking to scale, or you’re tired of wasting milk and money on off-spec batches, it’s a no-brainer. I always tell new customers to start small – maybe install one on your raw milk receiving line first, or your finished milk blend line, see how it works for you, then add more. No need to overhaul your entire system at once.
Another thing a lot of people don’t talk about: regulatory stuff. The FDA and other food safety agencies require accurate testing for dairy products to ensure they meet standards for fat, solids, and other components. In-line density meter data is already accepted by most regulatory bodies as a valid testing method, because it’s precise and consistent. So you don’t have to worry about failing an audit because your manual lab tests don’t match up – the meter’s data is logged automatically, so you can pull it up anytime for inspectors. That’s a huge win for plant managers, who spend way too much time prepping for audits.
I get it, switching to new equipment can be intimidating. When we first started selling in-line density meters to dairy plants, we had a customer who was convinced it would be too complicated to integrate with their existing PLC (programmable logic controller) system. But we send our technicians on site to install it, calibrate it, and train your staff in like a day. No coding required, no fancy software – it hooks up to your existing control system via standard Modbus or Ethernet, which most dairy plants already use. And our meters are built to last – we’ve had some customers who’ve had the same meter running for 10 years with only routine calibration every 6 months, which is way cheaper than hiring a lab tech full time or wasting product on off-spec batches.
Let’s address the counterpoints I’ve heard a hundred times. “What if the meter breaks?” Every meter comes with a 2-year warranty, and we keep spare parts on stock for all our customers. Also, we have remote monitoring, so if there’s a issue with the sensor, we can see it right away and walk your maintenance team through fixing it, no need to send someone out on a emergency trip. That’s a huge plus, especially for rural dairy operations that are far from service techs. And “we already use ultrasonic testing for density?” Ultrasonic is fine, but it’s less precise than the vibrating tube in-line meter, and it’s way more prone to interference from foam or air bubbles, which are super common in dairy lines. We’ve had customers switch from ultrasonic to our vibrating tube meters and see a 0.5% improvement in fat blend accuracy, which adds up over thousands of gallons.
At the end of the day, dairy is a margins game. Every gallon of milk that’s wasted, every hour of labor spent on manual testing, every batch that’s off-spec and sold for less – that’s money leaving your pocket. An in-line density meter isn’t just a piece of equipment; it’s an investment that pays for itself in 6-12 months, depending on your production volume. I’ve seen customers make back their entire investment in just 3 months because they caught one bad milk load or fixed a curd yield issue.
If you’re tired of the old way of doing things – waiting for lab results, wasting product, dealing with inconsistent batches, or worrying about audit fines – let’s talk. I don’t do pushy sales stuff, I just know what works for dairy operations because I’ve worked with hundreds of them over the years. Whether you’re a 5,000-gallon-a-day creamery or a 100,000-gallon-a-day plant, we can customize a solution that fits your needs, no one-size-fits-all garbage.

Don’t keep spinning your wheels with outdated testing methods. In-line density meters aren’t a trend – they’re a standard for modern dairy operations, and they’ll only get more important as demand for consistent, high-quality dairy products goes up. Reach out, and we can chat about your specific pain points and how a density meter can help.
Magnetostrictive Level Gauge References
- Morrison, S. C. (2021). Real-Time Process Monitoring in Dairy Manufacturing: A Review. Journal of Food Engineering, 298, 110452.
- International Dairy Federation. (2019). In-Line Sensory Technologies for Dairy Production Bulletin 485. IDF, Brussels.
- American Dairy Science Association. (2022). Process Control Technologies for Improved Dairy Yield and Quality. Journal of Dairy Science, 105(5), 4129-4141.
Shandong Aipuxin Automation Instrument Co., Ltd.
Shandong Aipuxin Automation Instrument Co., Ltd. is one of the most professional in-line density meter manufacturers and suppliers in China, specialized in providing high quality customized service. We warmly welcome you to wholesale cheap in-line density meter in stock here from our factory. For price consultation, contact us.
Address: Huigu Phase 1, Zhongnan High-tech Canal New City, Rencheng District, Jining City, Shandong Province
E-mail: aipuxin0124@gmail.com
WebSite: https://www.aipxin.com/
